
 Key Takeaways
- Tier-1 support: Delivering precision shop-floor documentation for mission-critical premium-OEM components (CT302 series).
- Metrology and quality: Developing measurement instructions for surface roughness (Rauhtiefe) and pot height inspections.
- Process optimization: Adapting press setup instructions (PAR) to guarantee repeatable clamping force.
- Defect management: Compiling a Polish defect catalog for brazing faults to accelerate N.I.O. (scrap/rejection) detection.
- Technical cleanliness: Translating vacuum-assisted closed-loop alcohol degreasing procedures.
Challenge: Micrometer precision in operator language
The project for a Tier-1 supplier plant in Upper Austria tested our process engineering capabilities. My objective was to translate intricate engineering specifications into clear, shop-floor work instructions optimized for high-takt manufacturing. The primary hurdle was document diversity — spanning strict NDAs and supplier registration forms (SDF) to ultra-technical descriptions of TOX clinching (mechanical sheet joining) and degreasing plant maintenance protocols.
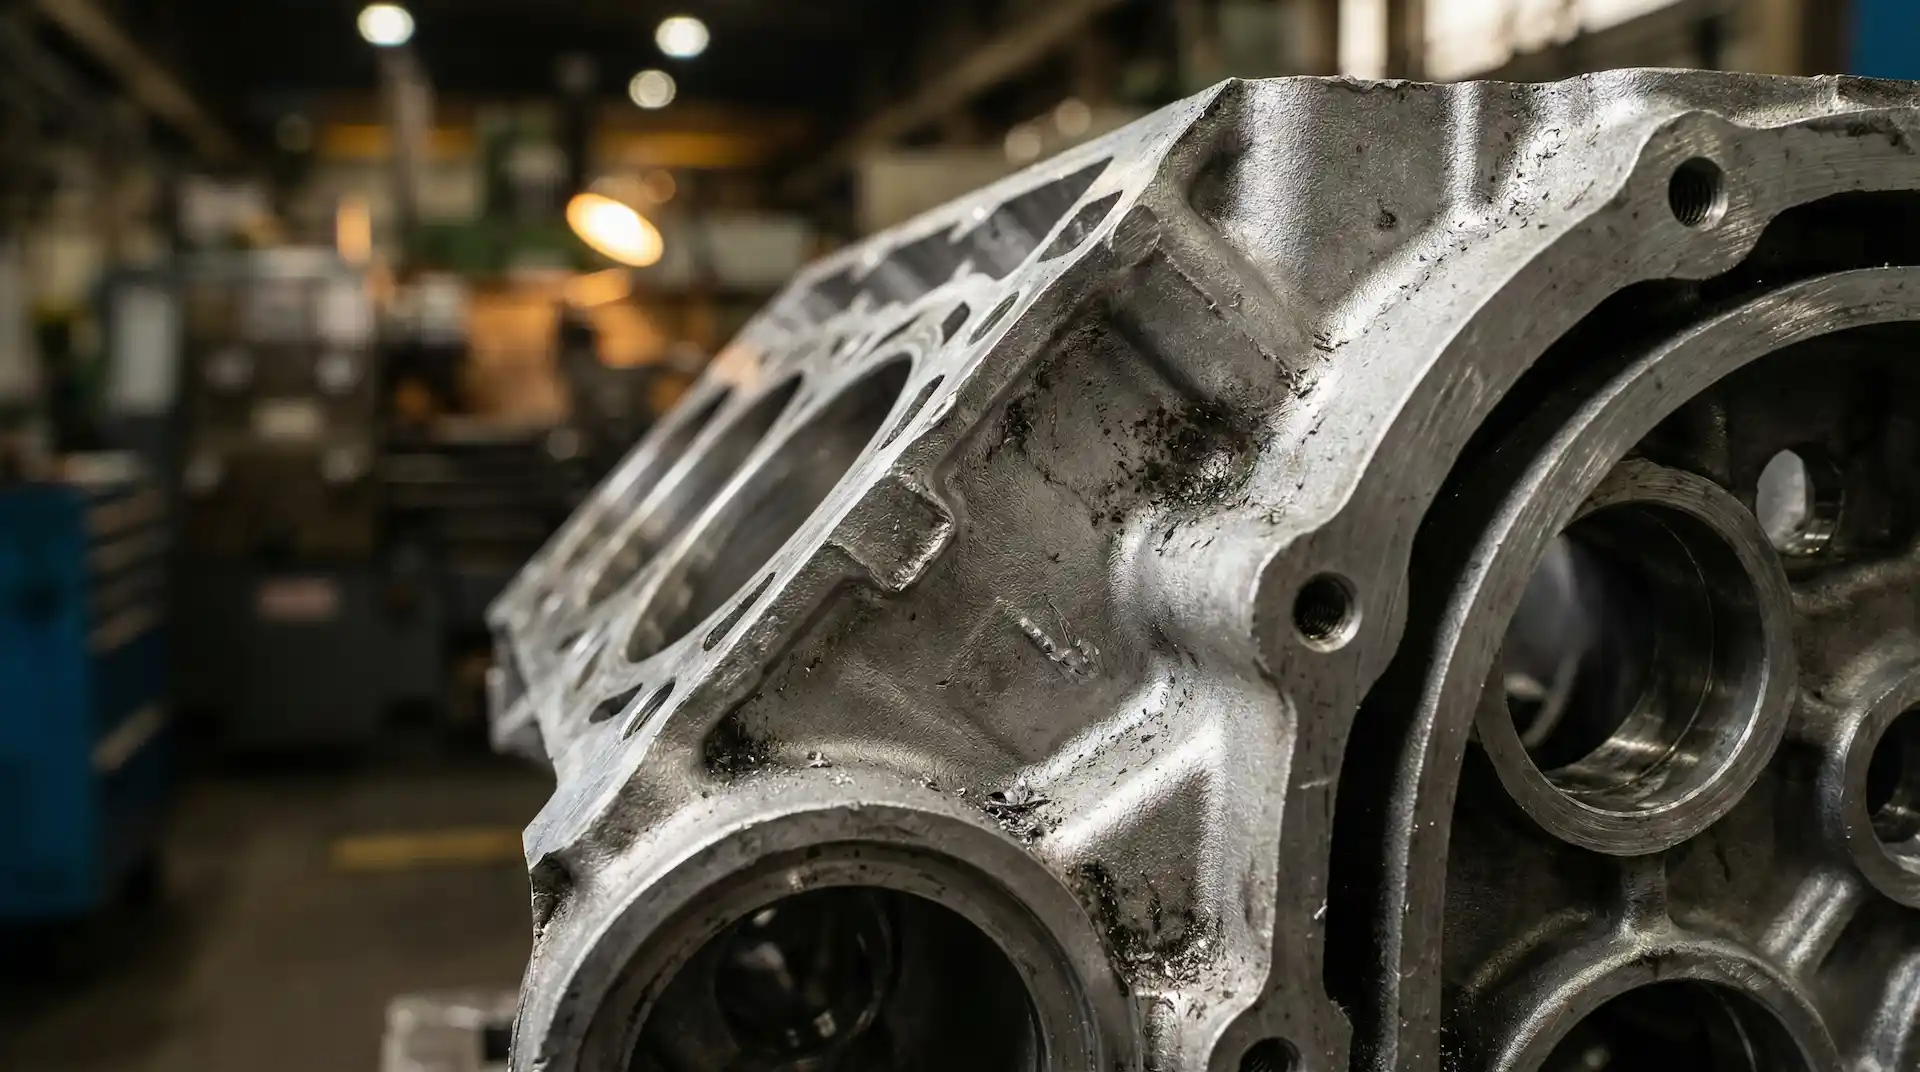
In manufacturing the CT302 series heat exchangers, every detail counts. The documentation covered key components including connection plates (Anschlussplatte) and cover plates for a premium OEM. Operators required a flawless understanding of Rauhtiefe (surface roughness) parameters and critical inspection points at differential pressure testing stations, where micro-leaks immediately classify a component as N.I.O. (Nicht in Ordnung / Not in order).
Implementation: From press parameterization to shipping audits
The documentation rollout was structured across three core technological pillars:
- Machine parameterization (PAR): Developing precise setup instructions for press clamping pressure (Verpressanlage 1–5). Because a fraction of a bar alters heat exchanger geometry, terminology precision directly safeguarded against costly material loss.
- Technical cleanliness engineering: Adapting operational procedures for integrated SCHAAL washing units and alcohol degreasing systems. Documentation detailed the removal of residual swarf and coolant using compressed air — a mandatory prerequisite prior to furnace brazing.
- Metrological verification (PM): Building a practical knowledge base for operators conducting pot height (Topfhöhe) and surface roughness measurements on stationary gauges under IATF 16949 compliance.
Result: Quality standards verified by audit
The project concluded with a formal shipping audit (Versandaudit), validating part labeling and packaging within the standard KLT container system. Through consistent, technically flawless documentation, the plant achieved a seamless technology transfer while reducing operator error rates. This project demonstrated that technical communication in automotive isn't just about words — it defines tolerances, parameters, and functional safety for components operating in millions of vehicles worldwide.
Verified references